Explore our premier selection of commercial-grade food and beverage hardware. Manufactured utilizing advanced metallurgical casting, automated deep-drawing, and double-wall vacuum insulation techniques under certified ISO9001 and FDA/LFGB food safety protocols.
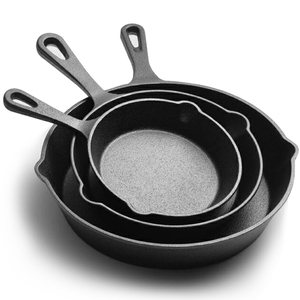
Precision-cast thermal retention pan designed for uniform induction heating and high-volume commercial catering endurance.
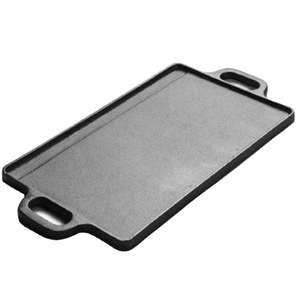
Engineered for extreme thermal storage and even heat distribution, ideal for outdoor commercial food service and BBQ exports.
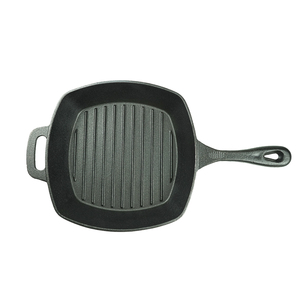
Commercial grade skillet featuring dual pour spouts and ergonomic support handles tailored for high-temperature steak houses.
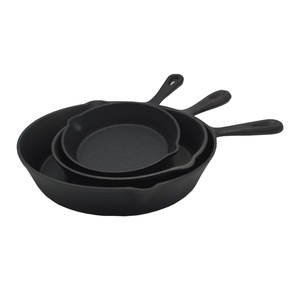
Complete wholesale combination set structured for retail packaging, global Amazon FBA distributors, and giftware lines.
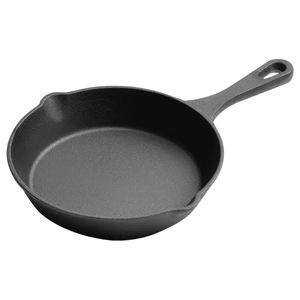
Rugged construction optimized for open fire camping, outdoor catering, and intensive commercial kitchen environments.
Multi-zone flat top griddle engineered with heavy carbon steel properties for rapid heat recovery in commercial diners.
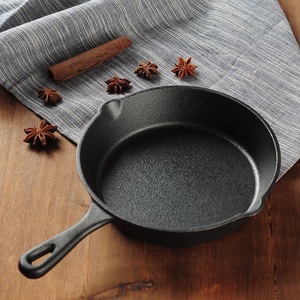
Industry benchmark cookware series featuring ultra-dense micro-textures for natural non-stick performance over time.
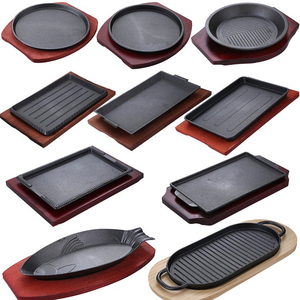
Specialized hospitality serveware designed to maintain sizzling plate temperatures directly from oven to table service.
In the highly competitive global drinkware sector, China wholesale vacuum insulated stainless steel tumbler manufacturers & exporters have redefined thermal efficiency standards through breakthroughs in vacuum degasification and multi-layer metallic bonding. Selecting the appropriate thermal vessel involves understanding the core metallurgical properties, vacuum pressure metrics, and surface chemistry required to deliver superior temperature retention and structural longevity.
Standard insulated drinkware utilizes double-wall construction, but premium B2B manufacturers employ specialized SUS304 (18/8 Austenitic Stainless Steel) for both inner liner and outer wall, or upgrade the inner fluid-contact vessel to SUS316 (18/10 Medical Grade Stainless Steel) for enhanced acid and chloride resistance.
The thermal insulation efficiency of a stainless steel tumbler is primarily determined by the quality of the vacuum space created between the inner and outer metal walls. Leading manufacturing facilities utilize continuous high-temperature vacuum brazing ovens operating at temperatures exceeding 500°C to pull vacuum levels down to 10-4 Pa.
To counteract radiative thermal exchange (the primary cause of heat loss across a vacuum barrier), high-performance tumblers incorporate an electroplated copper lining on the exterior side of the inner shell. This microscopic copper coating acts as a thermal mirror, reflecting up to 98% of infrared thermal radiation back into the contained liquid.
A common issue with low-tier wholesale drinkware is metallic leaching or odor retention. Advanced manufacturing processes incorporate multi-stage electrolytic polishing and chemical passivation. This removes free iron particles from the interior surface of the stainless steel, forming an ultra-clean, corrosion-resistant chromium oxide ($Cr_2O_3$) passive layer. This non-porous finish ensures zero flavor transfer when transitioning between acidic fruit juices, specialty coffee, and dairy beverages.
As corporate buyers, brand owners, and global importers navigate shifting supply chain dynamics, procurement strategies for stainless steel tumblers and commercial cookware are undergoing substantial shifts. Procurement managers must align with factories capable of adapting to the following four macro trends:
Regulatory frameworks across North America (such as state-level PFAS bans) and the European Union (REACH & Annex XVII updates) are making non-toxic surface treatments mandatory. Importers are transitioning from traditional liquid spray paints toward solvent-free electrostatic powder coatings. These provide superior scratch resistance (over 2H pencil hardness testing) while yielding zero volatile organic compounds (VOCs) during production.
Single-purpose push-on lids have been superseded by complex, dual-injection molded closure systems. Current procurement demand centers on 2-in-1 lid architectures that seamlessly switch between a high-flow sip opening and a integrated silicone straw. Lids manufactured from food-grade Eastman Tritan™ Copolyester ensure crystal clarity, impact toughness, and 100% BPA/BPS-free compliance.
Enterprise buyers require transparent material provenance. Advanced OEM/ODM factories implement spectral analyzer verification (XRF spectroscopy) at the raw steel coil stage, guaranteeing exact nickel and chromium concentrations prior to hydroforming, avoiding substandard scrap metal contamination.
The evolution of thermal drinkware closely mirrors advancements in cookware engineering. Technologies perfected in multi-ply stainless steel cookware—such as bonded aluminum core bases for rapid heat transfer—are now being adapted into thermal drinkware manufacturing line processes.
| Feature Spec | Standard Single-Wall Vessel | Commercial 304 Vacuum Tumbler | Premium Surgical 316 Copper-Lined |
|---|---|---|---|
| Inner Liner Grade | SUS 201 Stainless Steel | SUS 304 (18/8) Food Grade | SUS 316 (18/10) Surgical Grade |
| Insulation Tech | Air Gap (None) | Double-Wall Vacuum (10-3 Pa) | Double-Wall Vacuum + Radiant Copper Shield |
| Cold Retention (under 5°C) | < 2 Hours | 12 Hours | 24 to 36 Hours |
| Hot Retention (over 60°C) | < 1 Hour | 6 to 8 Hours | 12 to 18 Hours |
| Surface Finish | Basic Spray Paint | Standard Powder Coat | Tactile 3D UV Print / Ceramic Interior |
| Corrosion Resistance | Low (Risk of rust with acidic juices) | High (Standard Commercial Grade) | Ultra-High (Salt-Spray Tested > 96 Hours) |
Building upon over three decades of manufacturing excellence established since 1991, our production lines combine traditional metal-spinning craftsmanship with modern automated robotic welding systems. Spanning across extensive industrial facilities, our enterprise portfolio includes over 700+ active product designs distributed across 180+ global partners and dealers.
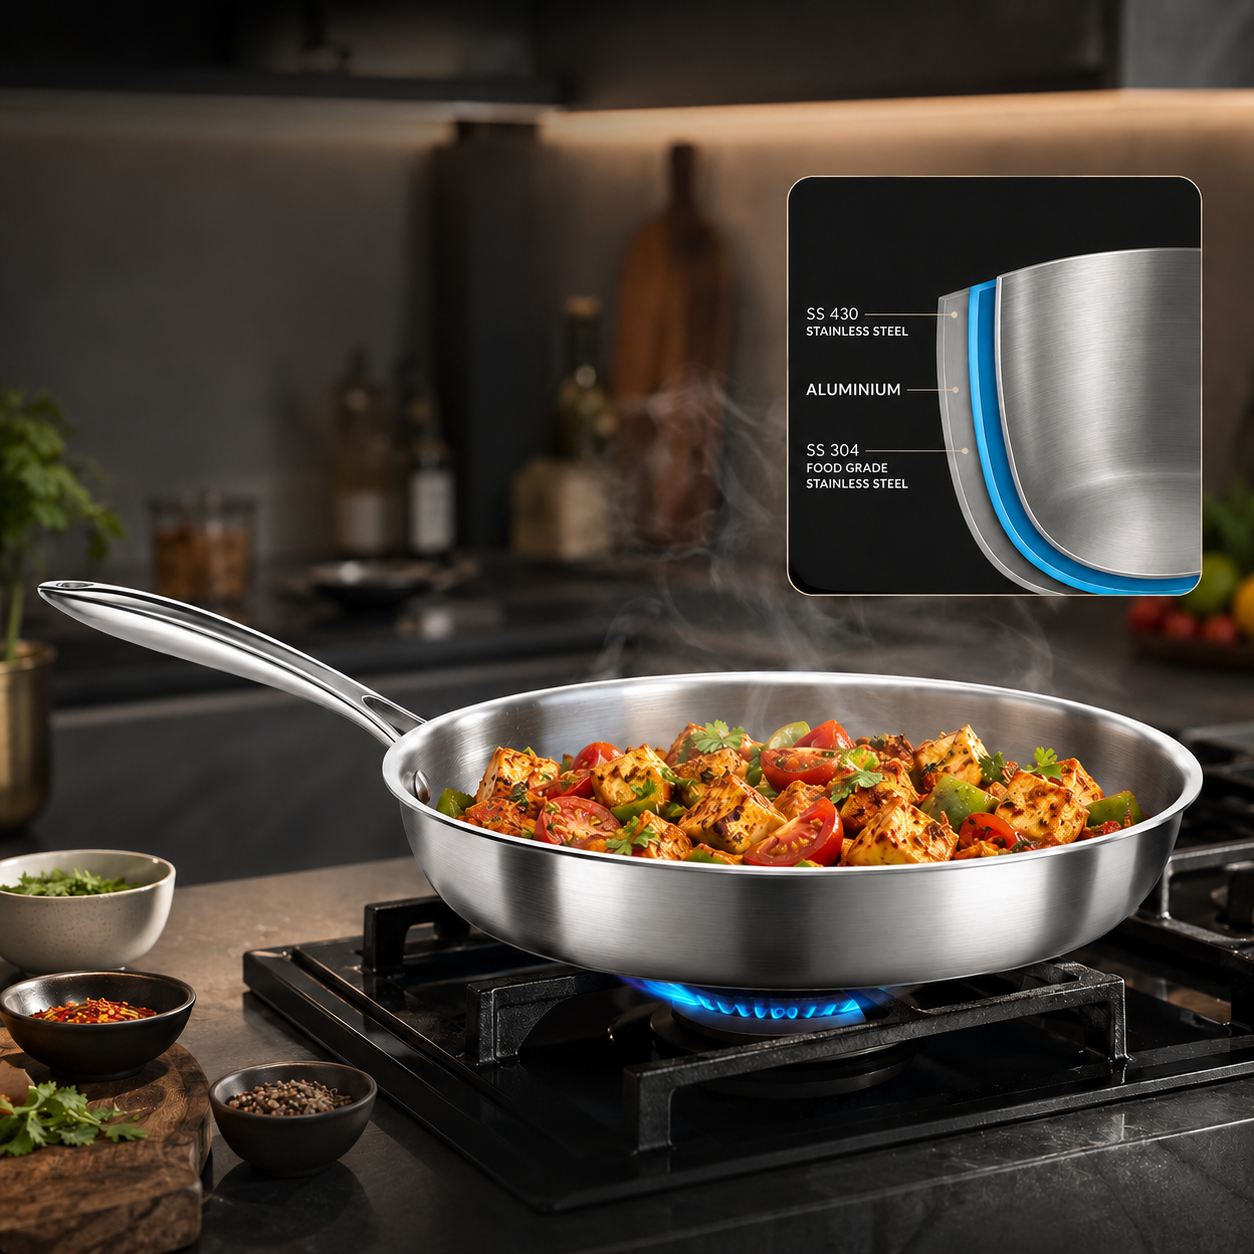
We source prime stainless steel coils backed by complete mill test certificates (MTC). Every batch undergoes rigorous spectroscopic testing to ensure nickel and chromium ratios strictly adhere to global food-contact safety parameters.
Every vacuum vessel passes through automated infrared temperature sensors post-brazing. Items failing to meet temperature retention thresholds within a 0.5°C margin are automatically ejected from the assembly line.
From initial 3D CAD modeling and custom lid mold development to laser etching, silkscreening, and retail box design, we provide complete end-to-end custom manufacturing for international brands.
Get clear, technical answers regarding minimum order quantities, manufacturing lead times, quality assurance standards, and custom OEM processes.
Our standard MOQ for custom color powder coating and laser-engraved branding starts at 1,000 units per color/design. For custom body shapes requiring new hydroforming tooling or unique lid injection molds, the base MOQ is typically 3,000 to 5,000 units depending on technical specifications.
All materials used in production—including stainless steel, silicone sealing rings, and Tritan™ plastic lids—are third-party tested and certified under FDA 21 CFR, EU 10/2011, LFGB, and REACH SVHC guidelines. Test reports from accredited laboratories (SGS, TUV, Intertek) are provided with master shipment documentation.
We test according to international standard EN 12546-1:2000. Tumblers are filled with 95°C water at an ambient temperature of 20°C ± 2°C. A pass result requires maintaining fluid temperatures above 65°C after 6 hours. For cold testing, 0°C ice water must remain below 10°C after 12 to 24 hours.
Yes. Standard unbranded stock samples are dispatched within 48 hours for quality evaluation. Custom prototype samples featuring your specified Pantone (PMS) powder coating, logo etching, and custom retail packaging require approximately 7 to 10 working days.
We offer an extensive selection of surface treatments: matte and glossy powder coats, metallic gradient spray, rubberized soft-touch coating, electropolished bare steel, 3D tactile UV printing, water transfer printing (marble/wood grain textures), and electroplated chrome finishes.
Standard mass production lead time is 30 to 35 days after sample approval and deposit confirmation. For re-orders with existing tooling, production can be expedited to 20 to 25 days. FOB, CIF, DDP, and EXW shipping terms are fully supported via sea, air, or express courier.
Our production lines implement a 100% 3-Stage Vacuum Inspection Protocol: First, immediately after vacuum brazing; second, post-powder coating baking; and third, prior to final automated packaging. We operate under strict AQL 1.5/4.0 inspection benchmarks.
We supply fully customized packaging solutions including 4-color offset printed corrugated boxes, cylinder gift tubes, window display boxes, custom EVA foam inserts, barcode labeling, and FBA outer carton palletization compliant with global retail fulfillment centers.