Engineered for maximum thermal efficiency, extreme durability, and food-grade hygiene. Custom OEM/ODM specifications available for global distributors and commercial buyers.
 Heavy-Duty
 Commercial Grade
 OEM Custom Logo
 Bestseller Set
 Dual Spout
 Square Modular
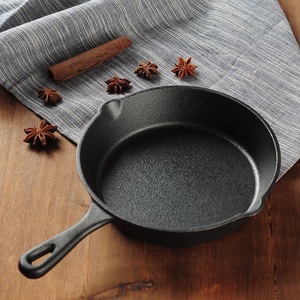 Industrial Grade
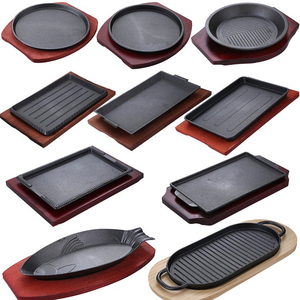 Custom Shape
Since 1991, our manufacturing infrastructure has set the industry standard for precision stainless steel engineering, vacuum insulation integrity, and international B2B wholesale distribution.
Our automated high-vacuum degassing chambers pull internal pressures down to 10⁻⁴ Pa, eliminating heat dissipation via convection and conduction for over 24 hours of temperature retention.
We source ultra-pure austenitic stainless steel with zero toxic leachates, complying with FDA 21 CFR, EU No 10/2011, and LFGB standards for non-reactive food safety under extreme thermal loads.
Full-spectrum custom manufacturing—ranging from 3D CAD rapid prototyping and custom hydraulic press tooling to laser logo engraving, custom color anodizing, and multi-layer retail packaging.
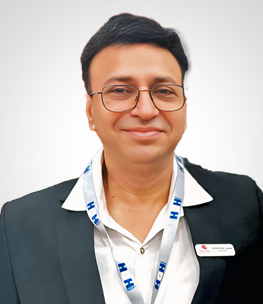
Under the executive leadership of Rakesh Jain (CEO) and Anmol Jain (Managing Director), Sorabh Kitchen World has evolved from a premier domestic manufacturer into a dominant exporter in the global stainless steel food container and insulated thermal transport sector.
By pairing legacy metalwork techniques with automated robotic laser seam welding and double-walled copper lining processes, our manufacturing plants output thousands of food carriers daily, serving institutional catering, military logistics, hospitality chains, and retail consumer brands worldwide.
In modern commercial food transport, maintaining thermal energy integrity over prolonged periods without external power inputs requires meticulous thermodynamic design. Insulated stainless steel food carriers prevent thermal degradation by targeting all three heat transfer mechanisms: Conduction, Convection, and Radiation.
1. Double-Wall Vacuum Chamber Isolation: The structural core of our food carrier consists of an inner food-contact shell and an outer protective shell. After robotic perimeter laser welding, the sealed assembly undergoes high-temperature vacuum degassing at 500°C in high-vacuum ovens. This evacuates residual gas molecules, completely cutting off conductive thermal pathways.
2. Interior Copper-Reflective Coating: Radiant heat loss is mitigated by electro-plating an ultra-thin radiant reflection copper layer onto the exterior of the inner SUS304 container. This metallic barrier reflects infrared heat radiation back into the food mass, significantly extending thermal retention curves.
| Steel Grade Standard | Chemical Composition (Cr / Ni / Mo) | Corrosion Resistance (PREN) | Thermal Stability Range | Recommended B2B Application |
|---|---|---|---|---|
| SUS304 (18/8 Austenitic) | 18% Cr / 8% Ni / 0% Mo | PREN ~19.0 | -196°C to +800°C | Standard Insulated Carriers, Soups, Rice, Dry Food Containers |
| SUS316 (18/10 Acid-Resistant) | 16-18% Cr / 10-14% Ni / 2-3% Mo | PREN ~23.0 to 25.0 | -196°C to +870°C | High-Acid Stews, Saline Solutions, Commercial Sauces & Pickles |
| SUS201 (Economical Grade) | 14-16% Cr / 1.5-3.5% Ni / High Mn | PREN ~13.5 | -20°C to +400°C | Outer Shell Enclosures, Outer Casing Components |
3. Thermal Decay Benchmark Profile: Under standardized test conditions (ambient room temperature of 20°C ± 2°C, initial liquid fill at 98°C), our heavy-duty insulated carriers demonstrate the following thermal decay performance:
As global supply chains place greater emphasis on sustainability, hygiene compliance, and cold/hot chain traceability, enterprise sourcing managers must align their supply lines with critical technological shifts currently transforming China's manufacturing sector.
Next-generation commercial food carriers feature integrated digital temperature displays, Bluetooth low-energy (BLE) sensors, and RFID asset tracking embedded into high-impact silicone and polypropylene (PP) lids, enabling logistics managers to monitor internal temperatures in real-time during transit.
Driven by the European Union's Carbon Border Adjustment Mechanism (CBAM) and corporate ESG quotas, leading suppliers are shifting toward eco-certified stainless steel billets (SS304-R) containing up to 80% post-consumer recycled metal, reducing scope 3 carbon intensity by 45%.
Advanced deep-drawing and internal hydroforming allow manufacturers to reduce inner shell wall thickness from 0.6mm to 0.35mm without sacrificing structural hoop strength, decreasing total transport weight by up to 25% for urban meal delivery fleets.
For B2B buyers, partnering with a Chinese supplier that proactively integrates these smart features and low-carbon metallurgical processes ensures product longevity and compliance with upcoming international commercial catering regulations.
The manufacturing process of high-grade insulated stainless steel food containers has shifted from manual labor-intensive assembly to fully integrated, automated smart factories. The technological roadmap includes several key developments:
Essential guidance for B2B procurement managers, catering equipment importers, and private label brand owners.
Partner with China's leading OEM manufacturer of insulated stainless steel food carriers and commercial kitchenware. Get factory-direct pricing, technical drawings, and material certification packages today.